PUBLISHED MANUFACTURER CASE
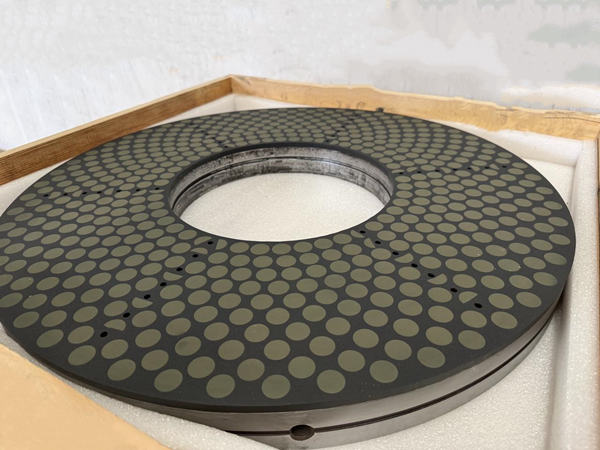
Valve-plate grinding on LAPMASTER DSG720
CategoryCustomer Cases
Published
EvidenceManufacturer report
Application context
The published case concerns CR2 steel valve plates on a LAPMASTER DSG720 with oil coolant and 0.12–0.15 mm stock removal. It reports 0.002 mm flatness and less than 0.004 mm parallelism; those results belong to this stated setup, not every workpiece.
Process, evidence & boundaries
The original publication provides the full process discussion and supporting context. Use it alongside the relevant product specification, and confirm the current configuration and workpiece requirements before placing an order.
| Item | Specification |
|---|---|
| Machine | LAPMASTER DSG720 |
| Spindle power | Upper disc 5.5 kW / Lower disc 5.5 kW / Center 3 kW |
| Workpiece | Valve plate |
| Material | CR2 steel |
| Hardness | 20 HRC |
| Workpiece size | Ø120 mm |
| Coolant | Oil |
| Stock removal | 0.12 - 0.15 mm |
| Cycle time requirement | < 3 minutes |
| Pre-finishing process | Casting |
| Surface roughness before finish grinding | 6 RZ |
| Surface roughness after finish grinding | 3 RZ |
| Flatness after finish grinding | 0.002 mm |
| Parallelism after finish grinding | < 0.004 mm |
| TTV (total thickness variation) | < 0.001 mm |
Reported surface and geometry results apply to the CR2 valve-plate setup above. The cycle entry is a stated requirement, not a measured guarantee for all production.